How to Build a Truck Flatbed
Sunday, August 30, 2026

A steel flatbed for a pickup costs between four and eight thousand dollars if you buy one. The steel to build one runs a few hundred. That gap is why flatbed builds are one of the best paying jobs a small metal shop can take on, and why a guy with a welder, a plasma table and a weekend can turn a rusted-out truck bed into real money.
I built one for a 2011 Dodge and filmed every stage of it. This is the written companion to that series — the whole build in order, what each stage actually involves, and the decisions that are easier to get right the first time than to fix later.
Fair warning up front: this is a real fabrication project, not a craft project. You are building something that carries load down a public road. Everything below assumes you can weld a structural joint you would stand under.
Why flatbeds are worth building
The margin is genuinely good. Material cost on a standard single-wheel bed lands in the low hundreds. Retail on a comparable new bed is thousands. Even at a modest labour rate, the job pays.
The demand is steady and local. Farm trucks, work trucks, service trucks. A stock pickup bed is a bad shape for anybody who actually hauls things — it is narrow between the wheel wells, it has no side access, and the first time somebody drops a pallet in it, it is bent.
It shows off everything else you do. A flatbed is a rolling billboard. Cut the owner's ranch brand into the headache rack with your plasma table and you have advertised your shop to everyone behind them at every red light for the next ten years.
It is repeatable. The frame is the frame. Once you have built one, the second one takes half as long, and the fifth one you can quote from memory.
Design it before you cut anything
You can build a bed off a sketch on a scrap of cardboard. People do. But drawing it properly first saves steel, and it means you can quote the job with real numbers instead of a guess.
I model these in SolidWorks using the weldments toolset, which is built for exactly this — you draw a skeleton of lines, tell it what tube profile goes on each line, and it generates the whole structure with mitred joints and a cut list.
That cut list is the useful part. It tells you exactly how many feet of each size of tube you need, which means one trip to the steel supplier and very little offcut.
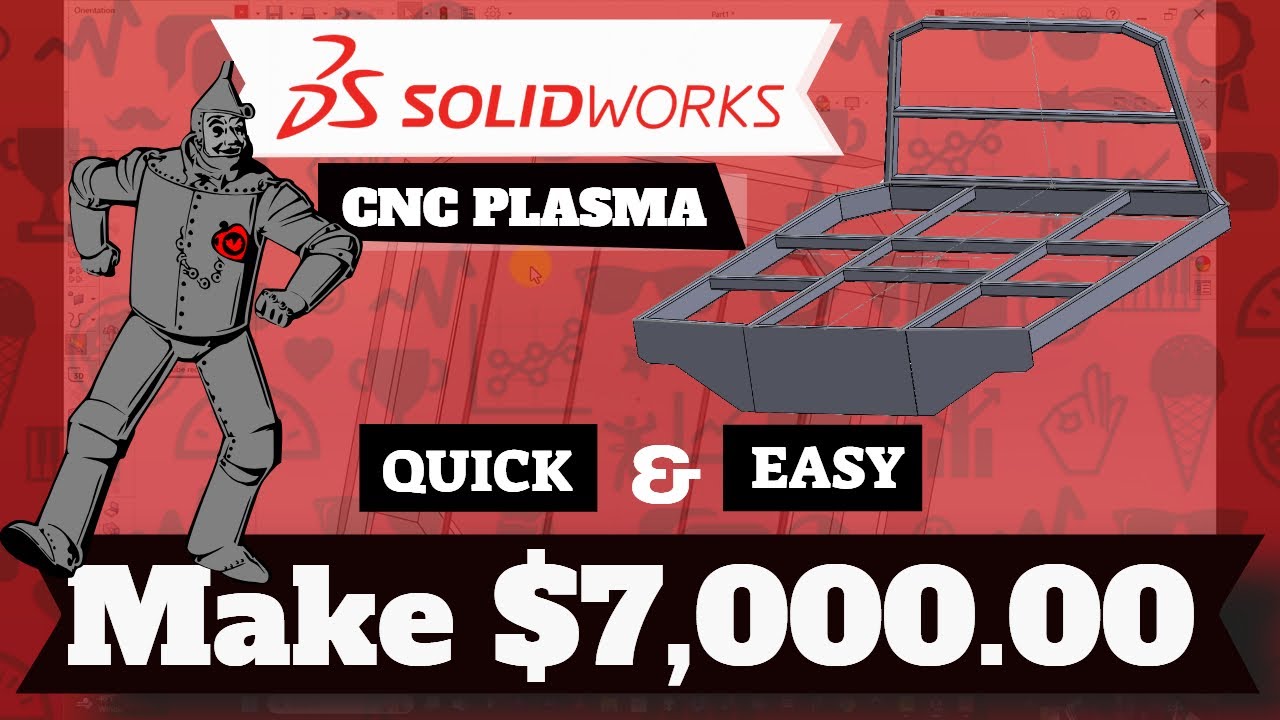
[Watch: How To Design A Truck Bed With Weldments in SolidWorks 2024](https://www.youtube.com/watch?v=aLQdJSpjS6s)
Fusion 360 has a similar workflow and is free for hobby use. Either works. The point is having a cut list before you have a pile of steel.
The tools you actually need
You do not need a fabrication shop. You need these:
- A welder with real duty cycle. MIG at 220V is the practical choice for structural tube. A 110V machine will run out of penetration on 3/16 wall and it will run out of duty cycle by lunchtime.
- A chop saw or a band saw. Every joint depends on square, repeatable cuts. A metal-cutting band saw pays for itself on the first bed.
- An angle grinder, and more flap discs than you think.
- Clamps. Far more than you own. Squares, magnets, vice grips, C-clamps. A flatbed is held together by clamps for two days before it is held together by welds.
- A flat surface to build on. This matters more than any tool on the list. A twisted bed will never sit right on the truck and you cannot fix it after the fact. A flat concrete floor works. A welding table is better.
- A plasma table, for the gussets, the brackets and the personalisation that turns a bed from generic into custom.
- Measuring gear and a big square. Measure the truck frame itself, not a spec sheet.
[Watch: Tools Needed For Truck Flat Bed Builds - all makes and models](https://www.youtube.com/watch?v=rLWkDp1rvtQ)
Stage 1 - Measure the truck and gather materials
The first video covers the measuring and the tooling for this specific truck, a 2011 Dodge.
The measurements that matter:
- Frame rail width, outside to outside, at the back of the cab and at the rear.
- Cab-to-axle distance. This is the number that decides bed length. Every manufacturer publishes it and every truck is slightly different from what is published, so measure it.
- Height of the frame rails relative to the cab, so the bed sits level and not nose-down.
- Where the fuel filler, the exhaust, the spare tyre winch and the wiring harness live, because all of those have to still work when you are done.
Take the old bed off first and photograph everything before you disturb it.
[Watch: How To Build A Truck Flatbed, Video 1 - tools you will need](https://www.youtube.com/watch?v=DsZqLSl1tX0)
Stage 2 - The main inner frame
This is the spine. Long rails running front to back, crossmembers between them, and the mounting points that tie it to the truck frame.
The things that decide whether this bed is good or scrap:
Build it square and keep it square. Measure the diagonals. If the two diagonal measurements across the rectangle are not identical, the frame is a parallelogram and nothing you do later will fix it.
Tack everything first, then measure, then weld. Tack the entire frame together. Check every diagonal and every dimension. Only then start laying real beads. A frame that was fully welded before it was checked is a frame you are cutting apart.
Weld in a sequence that balances the heat. Weld one long rail continuously and it will pull like a banana. Alternate ends, alternate sides, let it cool. This is the single biggest difference between a bed that sits flat and one that rocks.
Crossmember spacing follows the load. Closer spacing under where weight will actually sit. If this truck is carrying a bale spike or a welder, that is not a general-purpose bed and the frame under those points needs to reflect it.
[Watch: How To Build A Truck Flatbed, Video 2 - main inner frame](https://www.youtube.com/watch?v=j9SSmFKhHo8)
Stage 3 - The head piece
The head piece is the front section — the part that sits against the cab and, on most builds, carries the headache rack.
Two jobs: it stiffens the front of the bed, and it stops whatever you are hauling from coming through the back window.
Fitment is the whole game here. Too close and the cab and bed move against each other on a twist and something rubs through. Too far and it looks wrong and you have wasted deck length. Cab clearance also has to allow for the cab moving on its mounts, which it does, more than you would think.
This is also where a plasma table earns its keep. A headache rack is a flat panel that everybody sees. A ranch brand, a family name, a silhouette — that is a fifteen minute cut that turns a functional part into the reason the next customer calls you.
[Watch: How To Build A Truck Flatbed, Video 3 - head piece](https://www.youtube.com/watch?v=Dk9UKMEzWJw)
Stage 4 - Side rails
Side rails finish the perimeter, stiffen the deck edges and give you something to tie loads to.
Decisions to make before you cut:
Rub rail or flush? A rub rail standing proud of the deck protects the edge and gives you a natural place for tie-down pockets. Flush looks cleaner and loads slide off easier.
Stake pockets. Cheap to add now, impossible to add later, and they turn a flatbed into a bed that can have sides when it needs them.
Tie-downs. Put in more than you think you need and weld them to structure, not to sheet. A D-ring welded to a deck plate will tear the deck plate out. Welded to a crossmember it will not.
Lighting. Marker lights and tail lights have to be positioned and wired to be legal. Work out where the wiring runs before you weld the rails closed over the route it needs to take.
[Watch: How To Build A Truck Flatbed, Video 4 - side rails](https://www.youtube.com/watch?v=WZDILyFPmaE)
Stage 5 - Finish, mount and get paid
Decking, final welds, grinding, paint, and putting it on the truck.
Decking. Steel tread plate is durable and heavy. Wood is lighter, cheaper, easier to replace and a lot of farm customers prefer it. Ask the customer, do not assume.
Paint. Whatever you use, prep decides how long it lasts. Grind the mill scale off, degrease everything, prime it. A bed that rusts through at the welds in two years is a bed that costs you referrals.
Mounting. Bolt it to the frame rails using the factory holes where they exist. Do not weld a bed to a truck frame — welding on a frame rail changes the metal in the heat-affected zone and it is a real structural and liability problem.
Wiring. Lights, plug for a trailer, anything else. Do it properly with loom and grommets.
Then the part everybody actually cares about: what you charge. On a bed like this, the material is in the hundreds and the finished job is worth thousands. The number in the video title is not clickbait — the gap between what the steel costs and what the job is worth really is that wide.
[Watch: How To Build A Truck Flatbed, Video 5 - the finished bed](https://www.youtube.com/watch?v=B2feStC-Svo)
Being honest about the risk
Two things worth saying plainly.
Load ratings. A bed you built has no engineering certification on it. For a farm truck hauling hay, nobody is asking. For a commercial vehicle in a regulated fleet, they might, and rules on this vary by state and by what the truck is used for. Know which situation you are in before you take the job.
Insurance. If you are building these for customers and putting them on public roads, talk to your insurer. This is a different exposure than selling metal signs, and it is a five minute phone call.
Neither of those is a reason not to build flatbeds. Plenty of small shops do, profitably. They are a reason to know what you are standing in before you take money for it.
What to build first if you have never done one
Build one for yourself, or for a friend who will forgive you.
The first one will take three times as long as you planned. You will discover that your floor is not as flat as you thought, that heat pulls more than you expected, and that you needed twice as many clamps. All of that is cheap tuition on your own truck and expensive tuition on a customer's.
The second one, you will quote confidently.
Where the plasma table fits
A flatbed build is welding work, but the plasma table is what makes yours different from the one down the road: headache rack panels, gussets, brand plates, mounting brackets, custom tie-down plates, and the owner's name cut into the tailgate area.
If you want cut-ready artwork to drop into that headache rack, the [free CNC plasma cut file library](https://www.tinmanmetalworks.com/blog/free-cnc-plasma-cut-files) has designs in SVG and DXF at no cost, and the [store](https://www.tinmanmetalworks.com/hero-theme-store-front) has the rest.
And if the reason you are reading a flatbed article is that you are trying to work out how to make real money with metal, the [Tin Man Metal Works masterclass](https://www.tinmanmetalworks.com/start-today) is about exactly that — pricing, finding customers, and building a shop that pays, rather than a hobby that costs.
The short version
Model it first and get a cut list. Measure the truck, not the spec sheet. Build the inner frame dead square, tack everything before you weld anything, and balance your heat. Fit the head piece with real cab clearance. Put in more tie-downs than you think, welded to structure. Bolt it to the frame, never weld to it. And put your plasma work on the headache rack, because that is the part everybody sees.
Get E-Mail Notifications

Hi, I'm Charles Woten
Owner : Tin Man Metal Works
"Hey there! Thank you for visiting my blog—I hope this article provides some helpful insights and advice you can put to use right away. My goal is to give you the tools and knowledge you need to succeed. If you’d like to stay updated on future posts, feel free to join the mailing list at the bottom of the page.
Thank you again for being here. I want nothing more than to see you succeed and, ultimately, escape the rat race!"
Don't forget to sign up for blog notifications below if you found this article useful.

